banner
  • Unveiling the Precision Manufacturing Process of Non-Round Punches
    Unveiling the Precision Manufacturing Process of Non-Round Punches Oct 16, 2026
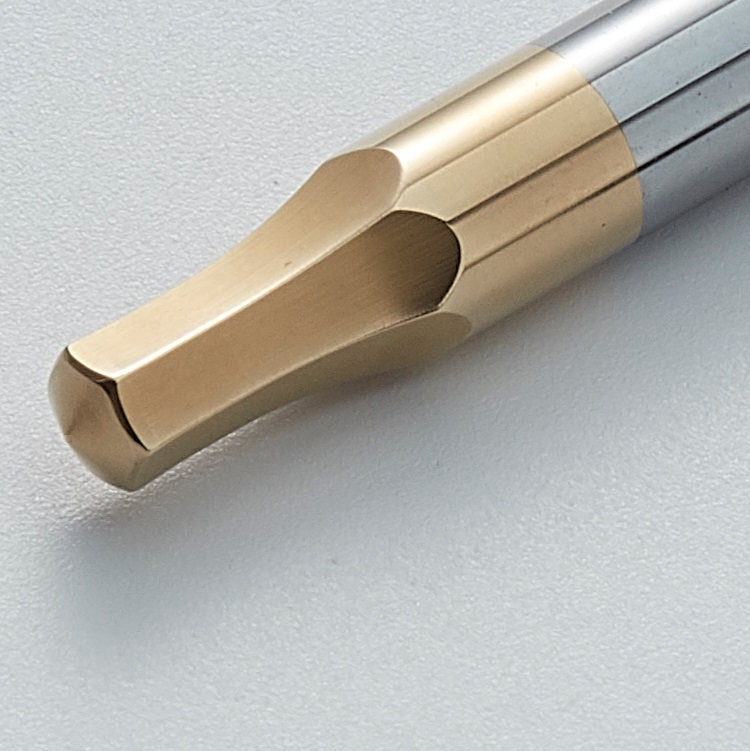
    In most people’s minds, a stamping die punch is just a simple round metal rod. However, in real-world modern manufacturing, a purely round shape is often no longer sufficient to meet increasingly complex design requirements. From polygonal locking holes in automotive connectors, to irregular slots in electronic terminals, and even special profiles with brand logos, these applications all rely on non-round punches (also called shaped punches).   As a professional die components manufacturer, HONGYU understands the critical role that non-round punches play in precision stamping. Today, we would like to take you deeper into the processing technology of non-round punches and reveal how hard steel can be ground into complex shapes with micron-level accuracy.   What Is a Non-Round Punch?   A non-round punch, as its name suggests, is a punch with a cross-section that is not perfectly circular. It breaks the limitation of traditional round punches and includes square, rectangular, oval, hexagonal, D-shaped, spline-shaped, and various custom irregular profiles. These punches are usually used to create holes with specific functional or mating requirements, and they are a core component in precision progressive dies and high-difficulty stamping applications.   Four Major Challenges in Non-Round Punch Processing   Compared with round punches, which can be easily processed by center-less grinding, the manufacturing difficulty of non-round punches increases dramatically. The main challenges are as follows:   1. Geometric Complexity Each non-round punch is essentially a new “creation.” Whether it is the transition between straight lines and arcs, or the connection between sharp corners and rounded corners, precise trajectory control is required. Any slight deviation may cause uneven clearance and affect stamping life.   2. Strict Dimensional Tolerance In precision stamping, the tolerance of non-round punches is often required to be controlled within ±0.005 mm. This means that over a length of dozens or even hundreds of millimeters, the dimensional variation must be less than one-tenth of the diameter of a human hair.   3. Sharp Corners and Radius Treatment Non-round punches often contain sharp corners or very small radii (R0.1–R0.5). These areas are prone to stress concentration or grinding burn during processing, which can lead to chipping and place extremely high demands on both the process and equipment.   4. Surface Finish Assurance Poor surface roughness can cause scratches, galling, or accelerated wear during stamping. Achieving a mirror finish below Ra 0.4 μm on a complex non-round cross-section is a major challenge in processing.   Our Core Processing Technologies   To overcome these challenges, HONGYU adopts a combined precision machining process, integrating multiple advanced machines to ensure that every non-round punch meets the highest requirements on the customer drawing.   1. Wire EDM – The Foundation of Complex Contours For extremely complex outer profiles or internal irregular holes, wire EDM is our first choice.   Advantage: Not limited by material hardness; even tungsten carbide with HRC 65 can be cut with ease. Precision: Positioning accuracy of up to ±0.003 mm, perfectly reproducing any CAD curve.  Application: Especially suitable for rough and semi-finish machining of tungsten carbide punches.   2. Optical Profile Grinding (PG) – The Final Guardian of Precision This is the core equipment for manufacturing high-precision non-round punches.   Principle: Through an optical projection system, the workpiece profile is enlarged 25x or 50x and projected onto a screen for comparison grinding against the standard profile. Features: Capable of precisely refining R corners and straightness, removing the machining marks left by wire EDM, and achieving extremely high dimensional accuracy and surface finish. Application: Suitable for small-batch, high-precision non-round punches and die insert processing.   3. CNC Jig Grinding – The Ultimate Solution for Internal Holes and Position Accuracy When machining precision internal holes in non-round punches, or when extremely high positional accuracy is required, CNC jig grinding becomes indispensable.   Function: Enables micron-level hole-position control and can machine high-finish internal holes in hard materials. Combination: Often used together with wire EDM — first cut the external shape, then perform precision internal-hole machining.   4. Combined Process and Coating – Performance Enhancement For the most demanding parts, we use a combined process:   First, rough shaping is done by wire EDM with a small machining allowance. Then, precision finishing is carried out by optical profile grinding or jig grinding to ensure dimensional accuracy and surface finish. Finally, based on customer requirements, surface coating such as TiN (gold), TiCN (blue-gray), CrN (silver), or DLC (black) can be applied to greatly improve wear resistance and anti-galling performance, thereby extending tool life.    Full-Process Quality Control   At HONGYU, every non-round punch must pass a strict inspection process before shipment:    Dimensional inspection: Critical contours and dimensions are 100% inspected using an automatic vision measuring system and a CMM.  Hardness inspection: Rockwell or Vickers hardness testing is used to verify whether heat treatment meets requirements.  Appearance inspection: The cutting edge is checked under a 20x microscope for chipping, cracks, or burrs. Trial fit verification: If necessary, the punch is trial-fitted with the matching die to ensure uniform clearance.   Case Study: Tungsten Carbide Non-Round Punch for Automotive Connectors   Customer Requirements:  Shape: Rectangle with a small radius corner (R0.2 mm)  Material: Tungsten carbide Tolerance: Width and length both controlled within ±0.005 mm  Lead time: Urgent order, delivery within one week     Faced with the high hardness of tungsten carbide and the requirement for a very small radius corner, we adopted a wire EDM precision cutting + optical profile grinding finishing solution. Wire EDM was used to ensure accurate external profile geometry, and PG grinding was then used to specifically refine the R corners and straight sections. Ultimately, a surface roughness of Ra 0.3 μm was achieved. The entire process was completed within 5 working days, and the part successfully passed the customer’s trial stamping verification.
  • 0.12 mm of Carbide, Zero Margin for Error: The Real Machining Story Behind Micro Tungsten Carbide Punches
    0.12 mm of Carbide, Zero Margin for Error: The Real Machining Story Behind Micro Tungsten Carbide Punches Sep 24, 2026
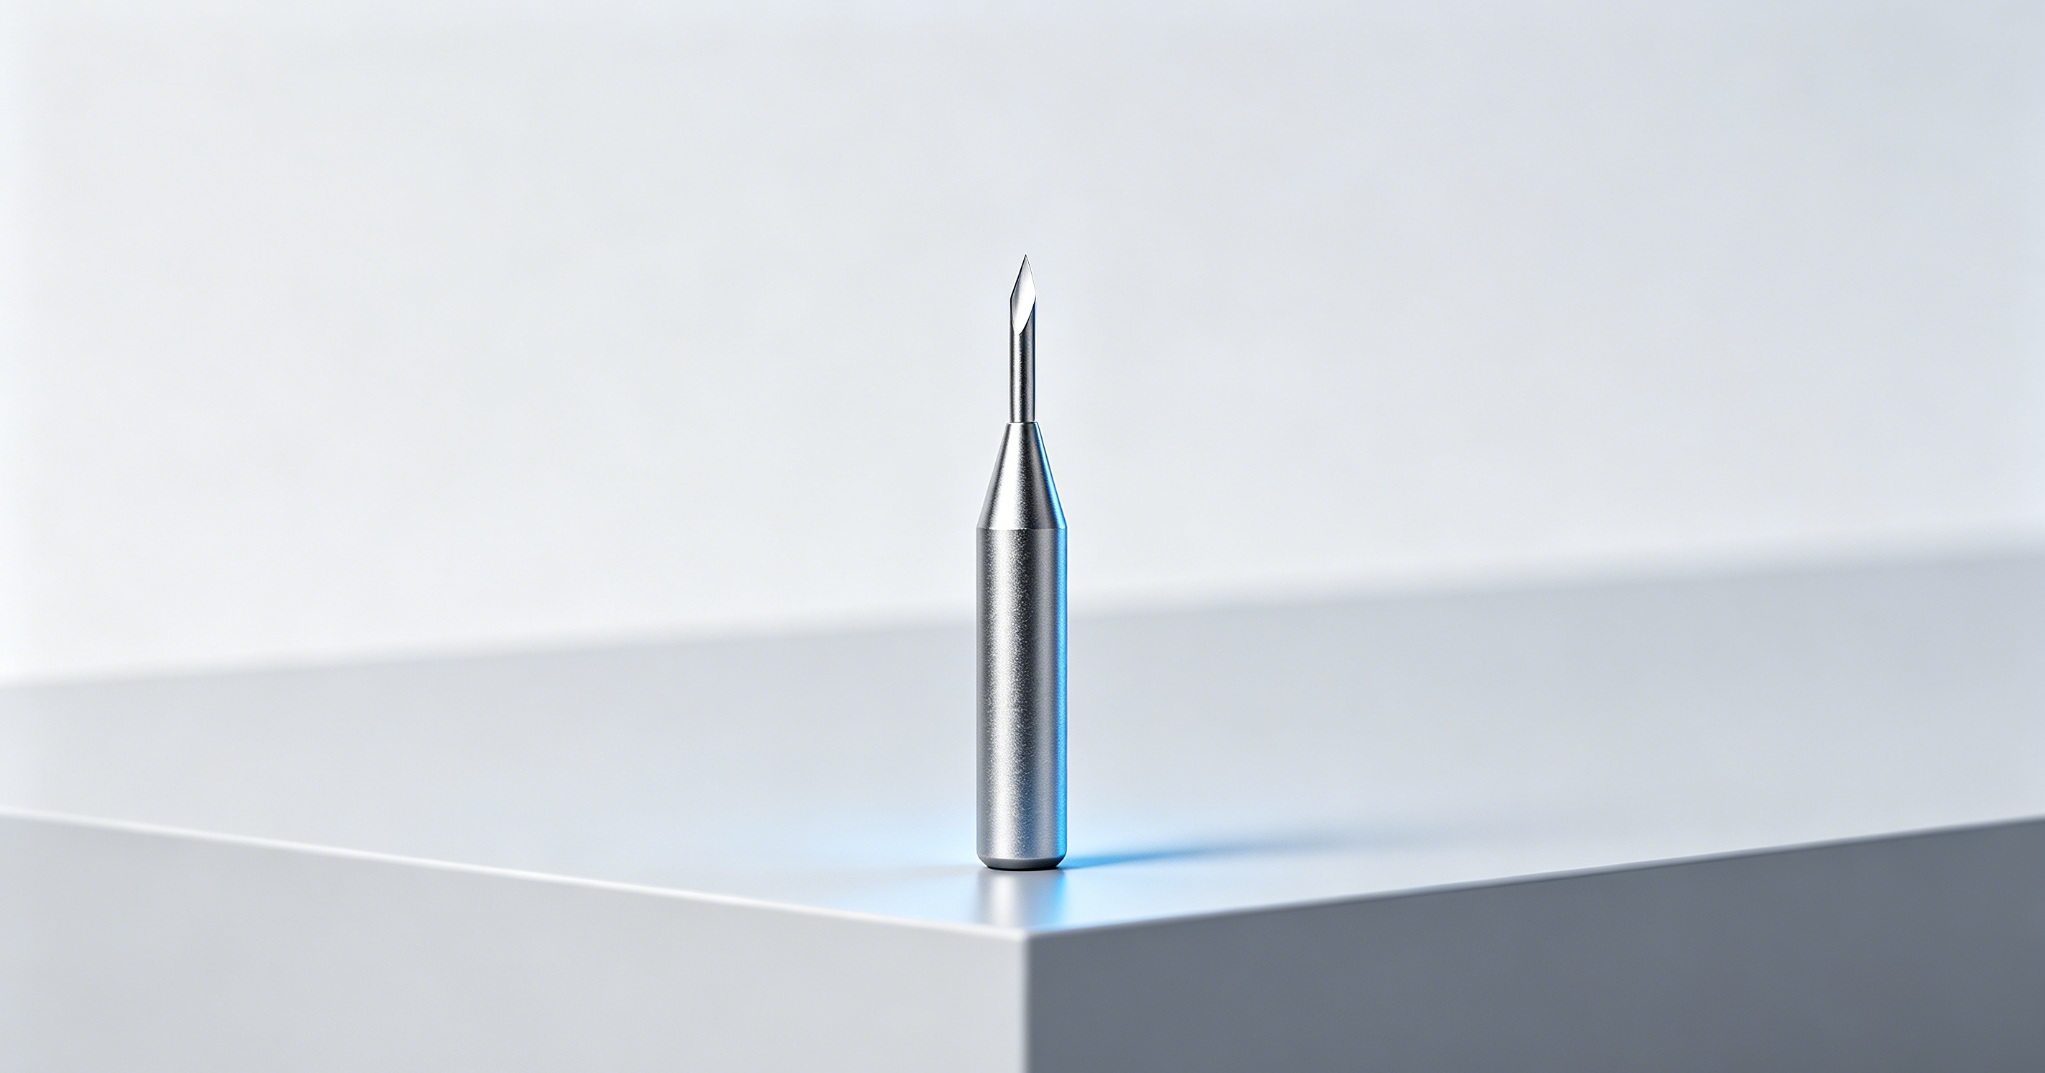
    In high end manufacturing sectors such as precision stamping and terminal & semiconductor connector molds, micro special shaped tungsten carbide punches are the critical core components that determine mould accuracy, finished part yield and service life. Compared with conventional high speed steel punches and standard round punches, micro special shaped tungsten carbide punches feature extremely high machining barriers, which can be described as a micron level precision craftsmanship test for mould part manufacturing.   Many mould manufacturers and precision engineering enterprises report that micro special shaped punches sourced from ordinary suppliers on the market are prone to chipped cutting edges, microcracks, dimensional deviations and short stamping lifespans, failing to meet the mass production requirements for high end precision applications. Today we take a typical high difficultity component — a 0.6 mm special profile punch with an ultra thin 0.12 mm cutting edge — as an example to thoroughly break down the core machining challenges, and reveal our proprietary process strengths that overcome industry pain points to consistently deliver ultra precision tungsten carbide punches. Inherent Material Conflict: ZeroTolerance Machining Dilemma under Extreme Hardness Tungsten carbide (cemented carbide) delivers exceptional hardness of HRA90 92 and outstanding wear resistance, making it the preferred material for micro precision punches suited for high frequency, continuous high precision stamping operations. However, it carries a critical material trade off: ultra high hardness paired with very low toughness and extreme brittleness.   For this micro special shaped punch with a 0.12 mm ultra thin cutting edge — as thin as a sheet of lightweight cardstock — the machining margin for error approaches zero. Minor machine tool vibration, slight deviations in grinding wheel feed parameters or tiny adjustments in clamping force can directly cause edge chipping or part fracture. Unlike high speed steel, which permits slight plastic yielding for stress buffering, tungsten carbide offers virtually no toughness buffer. Conventional machining processes are completely unsuitable for such ultra thin special profile structures, which explains why most small workshops cannot produce premium micro tungsten carbide punches.   Common Industry Pain Point: Hidden Defects Left by Wire EDM Machining Slow speed wire electrical discharge machining (Wire EDM) is widely used for rough shaping of micro special shaped punches. The electrical discharge process generates a recast metamorphic layer on the workpiece surface filled with invisible microcracks. These latent defects cannot be identified by visual inspection yet trigger rapid edge chipping and material spalling once the finished part runs on a stamping press, resulting in unplanned mould downtime and mass produced defective components.   The critical challenge in this process lies in ultra precise stock allowance control. For a 0.12 mm ultra thin cutting edge, the grinding allowance must be strictly maintained within a narrow window of 0.008 mm to 0.015 mm per side. Excessive stock removal will over thin the cutting edge and scrap the part; insufficient removal fails to fully eliminate the recast layer and leaves hidden quality risks. Most market side manufacturers rely on empirical settings with loose parameter control, unable to balance dimensional accuracy and service life, leading to low production yield. Core Craftsmanship Barrier: MicronLevel Optical Profile Grinding (PG) Technology After rough machining, final dimensional accuracy and cutting edge quality fully depend on Optical Profile Grinding (PG) — the core technical barrier for micro special shaped tungsten carbide punches and one of our key competitive advantages. Grinding ultra thin cutting edges differs drastically from standard punch fabrication. Every parameter and procedure is custom tuned:   1. Custom matched grinding wheels with frequent dressing: We deploy ultra fine grit diamond grinding wheels with custom dressing routines tailored to each special profile. High frequency precision dressing prevents edge chipping and profile distortion caused by wheel passivation, ensuring accurate forming of complex contours. 2. Micron scale intermittent feed control: Instead of conventional continuous tool paths, we adopt self optimised intermittent micro feed machining. Material removal per pass is limited to the micron range, eliminating grinding impact that would damage ultra thin cutting edges. Although cycle times are extended and productivity reduced, micro chipping and part deformation are reliably avoided. 3. Constant temperature stress relief machining system: Tungsten carbide exhibits poor thermal conductivity. Localised high grinding temperatures easily induce thermalstress microcracks. We deploy a dedicated thermostatically controlled cooling system with stabilised oil temperature and flow rate to eliminate thermally induced hidden cracks and preserve internal structural integrity. 4. Low stress custom tooling clamping: Tiny micro components risk crushing or positional shift during clamping. We utilise custom vacuum chucks and low stress fixtures for non deforming full contact clamping, preventing workpiece fracture, machining vibration and dimensional drift. Rigorous Quality Assurance: Multi Dimensional Inspection Standards Exceeding Industry Norms The value of premium micro tungsten carbide punches does not lie in producing visually acceptable prototypes. Real capability means stable mass production free of latent defects with consistent long term stamping performance. We implement a full process quality control standard stricter than typical industry requirements to resolve chronic industry issues such as inconsistent mass yield and after sales risks:   1. Precision control: Dimensional tolerances for special shaped profiles are stably held within ±0.003 mm, with perpendicularity ≤0.005 mm, meeting ultra high precision requirements for high end connector, semiconductor and precision terminal molds.   2. Microscopic inspection: 400× metallurgical microscopes are used for 100 % cutting edge inspection to eliminate notches and micro chips larger than 0.002 mm, detecting all invisible microscopic flaws.   3. Service life optimisation: Custom lightweight coating processes are developed for ultra thin cutting edge operating conditions, balancing sharpness and wear resistance. This avoids two common industry pitfalls: excessive coating thickness causing stamping burrs, and insufficient coating thickness shortening service life. 4. Mass production stability: Full process SPC dimensional monitoring guarantees consistent precision across batches, eliminating lot to lot variation to support customers’ large volume manufacturing. Our Core Competency: Turning “High Difficulty Non Standard Parts” into “Reliable Consistent Deliverables”   The current industry landscape shows overcapacity and fierce price competition for standard tungsten carbide punches. In contrast, high precision, micro sized, ultra thin and special shaped tungsten carbide punches remain in critically short supply among qualified suppliers due to demanding machining requirements, low yield rates and high technical barriers — representing a key urgent demand for high end mould manufacturers.   With years of expertise in precision mould part fabrication, we specialise in custom engineered high difficulty micro special shaped tungsten carbide punches. Our distinct strengths are summarised below:   ✅ Proven solutions for challenging applications including ultra thin cutting edges, micro structured profiles and slender micro punches   ✅ Self optimised integrated processes for Wire EDM stock allowance, PG grinding and stress controlled machining to eliminate microcracks, edge chipping and dimensional nonconformity   ✅ Full set of high precision equipment, custom tooling and strict quality control delivering mass yields well above industry averages   ✅ Customisation available for a full range of non standard micro special shaped tungsten carbide punches for precision stamping, terminal, semiconductor and medical device high end industries   The precision of mould components defines the quality of end products. Micron level process innovation builds core enterprise competitiveness. The manufacturing complexity of micro special shaped tungsten carbide punches represents an industry technical barrier — and our competitive advantage. We reject crude machining and latent defects. Adhering to the standards of micron level accuracy, zero microcracks, extended service life and consistent reliability, we help high end manufacturing customers resolve precision mould part bottlenecks, improve mould longevity, production yield and overall market competitiveness.   If you require custom high difficulty micro special shaped tungsten carbide punches and precision mould piercing tools, please feel free to contact us for your dedicated precision  machining solution.  
  • Three Core Priorities for Stamping Mold Business Owners in 2026
    Three Core Priorities for Stamping Mold Business Owners in 2026 Jun 06, 2026
    The stamping mold industry has moved past the era of relying on high output and low prices to win orders. In 2026, market homogeneity, rising raw material and labor costs, and increasingly strict customer inspection standards have reshaped the industry competition. It now focuses on stable quality, controllable profits and precise customer resources.   There is no need to chase impractical high-tech concepts or blindly expand production capacity. Focusing on these three practical tasks will help mold manufacturers stabilize their business and stand out from competitors. Prioritize Stable Quality, Abandon Unreliable Mass Production Whether for domestic key clients or foreign trade orders, customers value most is mold stability, fewer after-sales problems and worry-free mass production. Many mold factories have sufficient inquiries, yet lose profits and reputation due to repeated mold modifications, burrs, springback, deformation and inconsistent mold service life during production.   In 2026, quality competition is essentially standardized operation competition. We conduct thorough DFM review, precise layout and structural optimization in advance to avoid cracking, scratching and dimensional errors from the source. During production, we strictly control steel selection, heat treatment accuracy and edge polishing processes. Standardized mold testing is implemented to ensure consistent sample quality.   With solid craftsmanship and standardized workflows instead of fancy intelligent equipment, factories can greatly reduce defective rates, stabilize mold precision and service life — the core to retaining old customers and gaining new referrals.   Adopt Refined Cost Control, Avoid Extensive Profit Loss Industry profits have become highly transparent, and raising prices is no longer a feasible solution. Refined cost control equals profit growth. Many mold factories maintain a steady order volume but gain slim profits, mainly due to extensive cost management.   Successful mold owners focus on detailed cost control in every production link. Adopt standardized and modular mold bases to reduce redundant processing and material waste. Optimize processes upfront to cut repeated mold testing and modification costs. Standardize daily mold maintenance and regular replacement of vulnerable parts to extend mold service life and lower rework expenses.   We match materials and processes reasonably, avoiding excessive cost from over-specified materials and quality loss from cutting corners. Precise cost control is the key to securing profits amid fierce low-price competition. Upgrade Service & Select High-quality Tracks, Stop Blind Low-price Bidding The industry shows obvious polarization in 2026. Low-end orders only bring cutthroat price competition, while emerging tracks including new energy, precision electronics and foreign trade offer stable orders and better profits. Mold owners need to actively target high-value markets such as precision stamping, new energy structural parts and export-standard molds to avoid homogeneous low-end competition.   Meanwhile, enterprises must transform from simple mold suppliers to one-stop solution providers. We offer full-cycle services, including pre-production drawing evaluation and process optimization, mid-production manufacturing and trial testing, and post-production mass production support and after-sales maintenance. For foreign trade orders, we comply with international inspection standards and ensure traceable quality and complete compliance documents to expand overseas markets and get rid of price wars. There are no sudden windfalls in the 2026 stamping mold industry, only steady and down-to-earth development. Stabilize quality to lay a solid foundation, control costs to retain profits, and upgrade services to expand market share. By sticking to these three practical priorities, mold enterprises can survive industry reshuffling and achieve long-term stable growth.  

Need Help? Chat with us

leave a message
For any request of information or technical support, fill in the form. All fields marked with an asterisk* are required.
Submit
Looking for FAQs?
Contact us #
+86 769 832011519

Our hours

Mon 11/21 - Wed 11/23: 9 AM - 8 PM
Thu 11/24: closed - Happy Thanksgiving!
Fri 11/25: 8 AM - 10 PM
Sat 11/26 - Sun 11/27: 10 AM - 9 PM
(all hours are Eastern Time)

home

products

whatsApp

Contacts