banner
  • 0.12 mm of Carbide, Zero Margin for Error: The Real Machining Story Behind Micro Tungsten Carbide Punches
    0.12 mm of Carbide, Zero Margin for Error: The Real Machining Story Behind Micro Tungsten Carbide Punches Sep 24, 2026
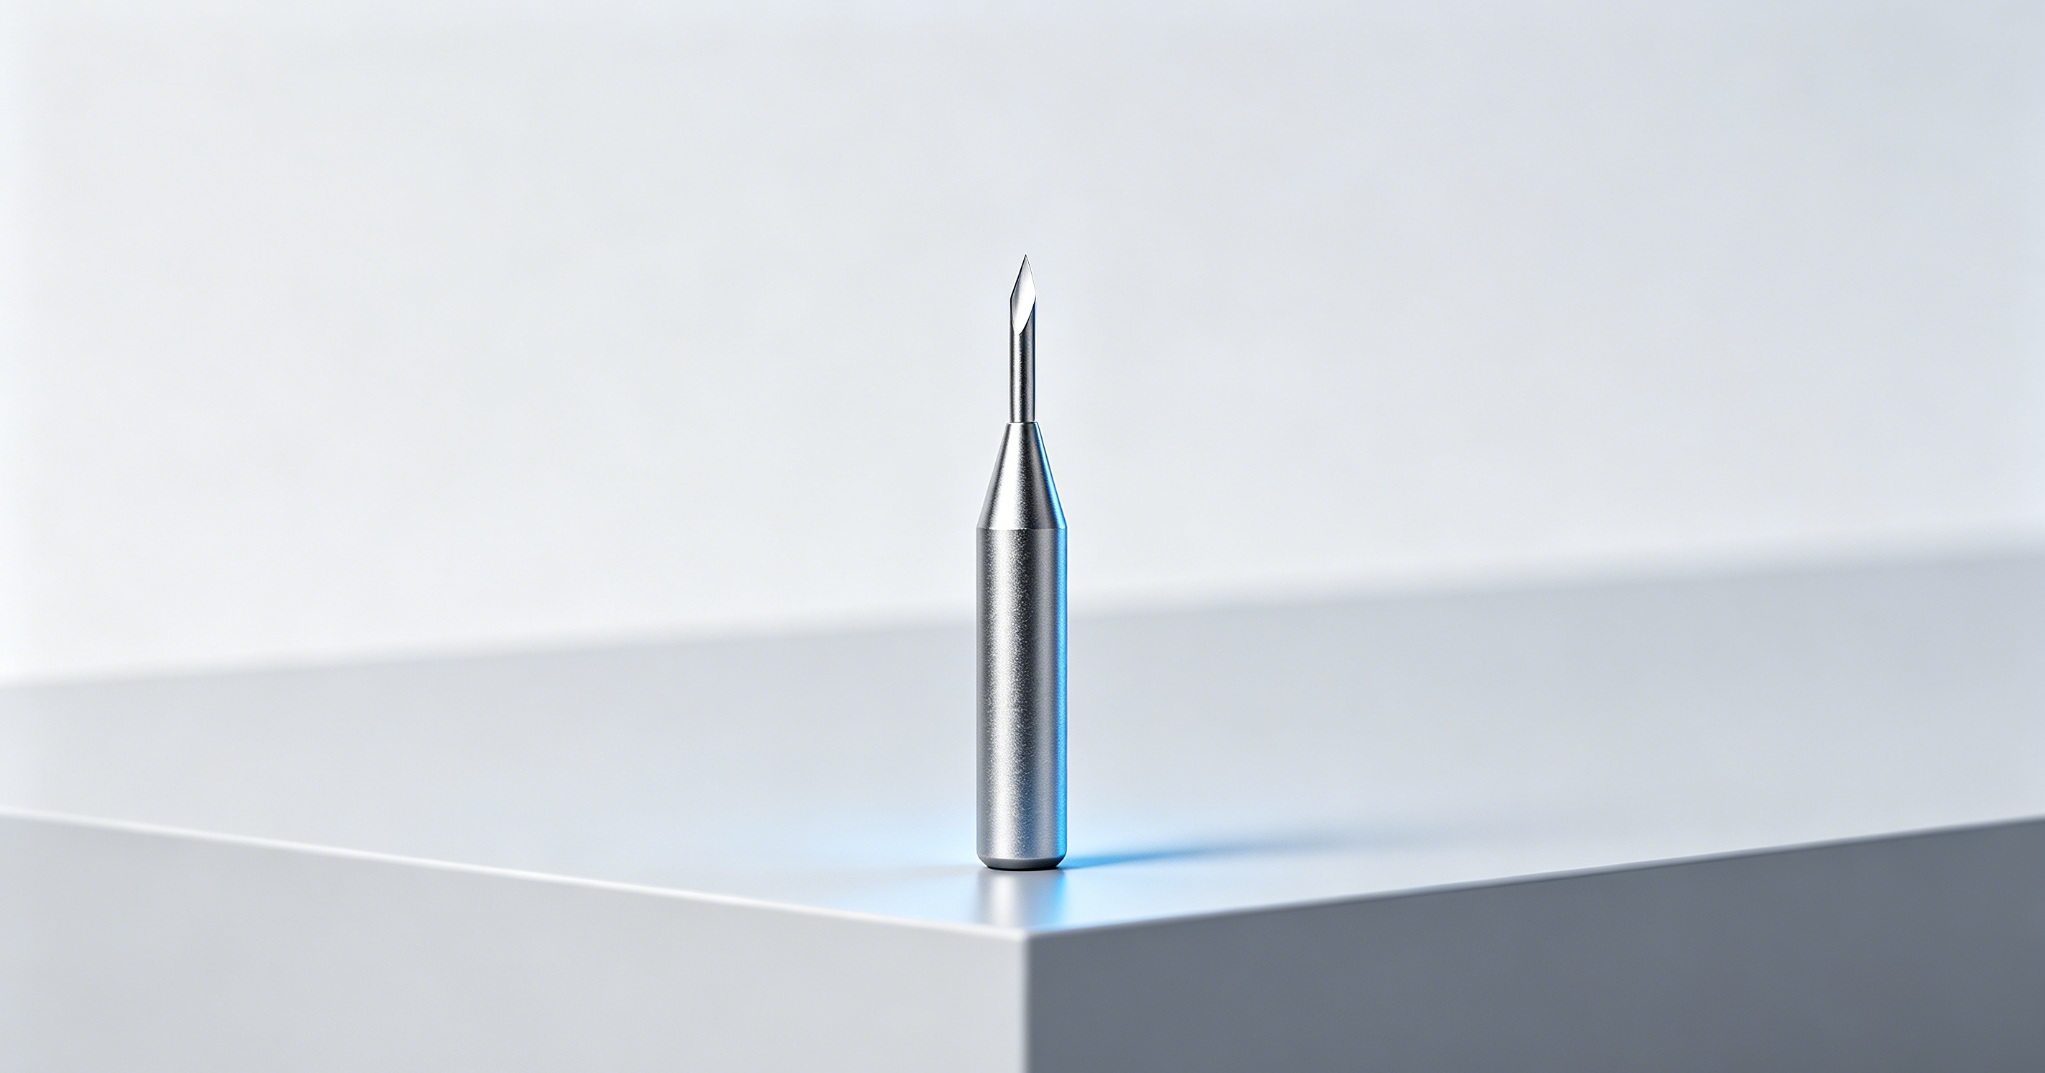
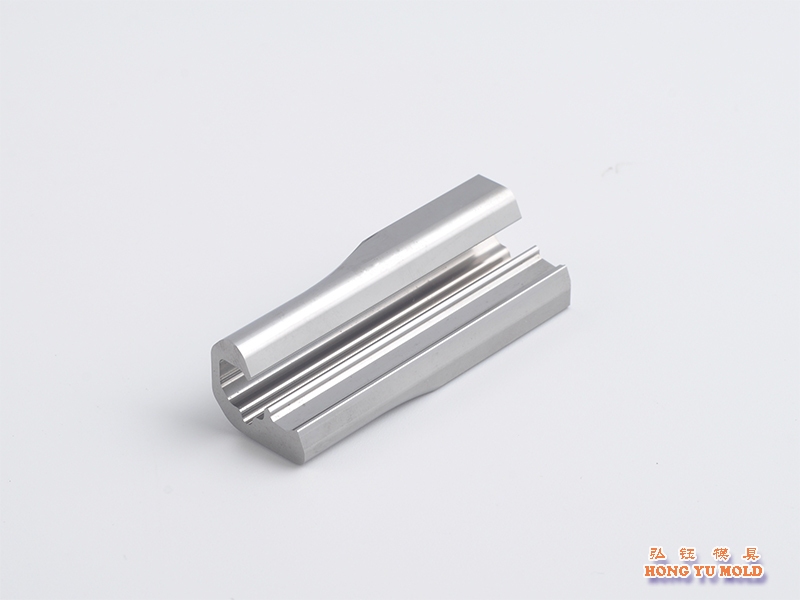
    In high end manufacturing sectors such as precision stamping and terminal & semiconductor connector molds, micro special shaped tungsten carbide punches are the critical core components that determine mould accuracy, finished part yield and service life. Compared with conventional high speed steel punches and standard round punches, micro special shaped tungsten carbide punches feature extremely high machining barriers, which can be described as a micron level precision craftsmanship test for mould part manufacturing.   Many mould manufacturers and precision engineering enterprises report that micro special shaped punches sourced from ordinary suppliers on the market are prone to chipped cutting edges, microcracks, dimensional deviations and short stamping lifespans, failing to meet the mass production requirements for high end precision applications. Today we take a typical high difficultity component — a 0.6 mm special profile punch with an ultra thin 0.12 mm cutting edge — as an example to thoroughly break down the core machining challenges, and reveal our proprietary process strengths that overcome industry pain points to consistently deliver ultra precision tungsten carbide punches. Inherent Material Conflict: ZeroTolerance Machining Dilemma under Extreme Hardness Tungsten carbide (cemented carbide) delivers exceptional hardness of HRA90 92 and outstanding wear resistance, making it the preferred material for micro precision punches suited for high frequency, continuous high precision stamping operations. However, it carries a critical material trade off: ultra high hardness paired with very low toughness and extreme brittleness.   For this micro special shaped punch with a 0.12 mm ultra thin cutting edge — as thin as a sheet of lightweight cardstock — the machining margin for error approaches zero. Minor machine tool vibration, slight deviations in grinding wheel feed parameters or tiny adjustments in clamping force can directly cause edge chipping or part fracture. Unlike high speed steel, which permits slight plastic yielding for stress buffering, tungsten carbide offers virtually no toughness buffer. Conventional machining processes are completely unsuitable for such ultra thin special profile structures, which explains why most small workshops cannot produce premium micro tungsten carbide punches.   Common Industry Pain Point: Hidden Defects Left by Wire EDM Machining Slow speed wire electrical discharge machining (Wire EDM) is widely used for rough shaping of micro special shaped punches. The electrical discharge process generates a recast metamorphic layer on the workpiece surface filled with invisible microcracks. These latent defects cannot be identified by visual inspection yet trigger rapid edge chipping and material spalling once the finished part runs on a stamping press, resulting in unplanned mould downtime and mass produced defective components.   The critical challenge in this process lies in ultra precise stock allowance control. For a 0.12 mm ultra thin cutting edge, the grinding allowance must be strictly maintained within a narrow window of 0.008 mm to 0.015 mm per side. Excessive stock removal will over thin the cutting edge and scrap the part; insufficient removal fails to fully eliminate the recast layer and leaves hidden quality risks. Most market side manufacturers rely on empirical settings with loose parameter control, unable to balance dimensional accuracy and service life, leading to low production yield. Core Craftsmanship Barrier: MicronLevel Optical Profile Grinding (PG) Technology After rough machining, final dimensional accuracy and cutting edge quality fully depend on Optical Profile Grinding (PG) — the core technical barrier for micro special shaped tungsten carbide punches and one of our key competitive advantages. Grinding ultra thin cutting edges differs drastically from standard punch fabrication. Every parameter and procedure is custom tuned:   1. Custom matched grinding wheels with frequent dressing: We deploy ultra fine grit diamond grinding wheels with custom dressing routines tailored to each special profile. High frequency precision dressing prevents edge chipping and profile distortion caused by wheel passivation, ensuring accurate forming of complex contours. 2. Micron scale intermittent feed control: Instead of conventional continuous tool paths, we adopt self optimised intermittent micro feed machining. Material removal per pass is limited to the micron range, eliminating grinding impact that would damage ultra thin cutting edges. Although cycle times are extended and productivity reduced, micro chipping and part deformation are reliably avoided. 3. Constant temperature stress relief machining system: Tungsten carbide exhibits poor thermal conductivity. Localised high grinding temperatures easily induce thermalstress microcracks. We deploy a dedicated thermostatically controlled cooling system with stabilised oil temperature and flow rate to eliminate thermally induced hidden cracks and preserve internal structural integrity. 4. Low stress custom tooling clamping: Tiny micro components risk crushing or positional shift during clamping. We utilise custom vacuum chucks and low stress fixtures for non deforming full contact clamping, preventing workpiece fracture, machining vibration and dimensional drift. Rigorous Quality Assurance: Multi Dimensional Inspection Standards Exceeding Industry Norms The value of premium micro tungsten carbide punches does not lie in producing visually acceptable prototypes. Real capability means stable mass production free of latent defects with consistent long term stamping performance. We implement a full process quality control standard stricter than typical industry requirements to resolve chronic industry issues such as inconsistent mass yield and after sales risks:   1. Precision control: Dimensional tolerances for special shaped profiles are stably held within ±0.003 mm, with perpendicularity ≤0.005 mm, meeting ultra high precision requirements for high end connector, semiconductor and precision terminal molds.   2. Microscopic inspection: 400× metallurgical microscopes are used for 100 % cutting edge inspection to eliminate notches and micro chips larger than 0.002 mm, detecting all invisible microscopic flaws.   3. Service life optimisation: Custom lightweight coating processes are developed for ultra thin cutting edge operating conditions, balancing sharpness and wear resistance. This avoids two common industry pitfalls: excessive coating thickness causing stamping burrs, and insufficient coating thickness shortening service life. 4. Mass production stability: Full process SPC dimensional monitoring guarantees consistent precision across batches, eliminating lot to lot variation to support customers’ large volume manufacturing. Our Core Competency: Turning “High Difficulty Non Standard Parts” into “Reliable Consistent Deliverables”   The current industry landscape shows overcapacity and fierce price competition for standard tungsten carbide punches. In contrast, high precision, micro sized, ultra thin and special shaped tungsten carbide punches remain in critically short supply among qualified suppliers due to demanding machining requirements, low yield rates and high technical barriers — representing a key urgent demand for high end mould manufacturers.   With years of expertise in precision mould part fabrication, we specialise in custom engineered high difficulty micro special shaped tungsten carbide punches. Our distinct strengths are summarised below:   ✅ Proven solutions for challenging applications including ultra thin cutting edges, micro structured profiles and slender micro punches   ✅ Self optimised integrated processes for Wire EDM stock allowance, PG grinding and stress controlled machining to eliminate microcracks, edge chipping and dimensional nonconformity   ✅ Full set of high precision equipment, custom tooling and strict quality control delivering mass yields well above industry averages   ✅ Customisation available for a full range of non standard micro special shaped tungsten carbide punches for precision stamping, terminal, semiconductor and medical device high end industries   The precision of mould components defines the quality of end products. Micron level process innovation builds core enterprise competitiveness. The manufacturing complexity of micro special shaped tungsten carbide punches represents an industry technical barrier — and our competitive advantage. We reject crude machining and latent defects. Adhering to the standards of micron level accuracy, zero microcracks, extended service life and consistent reliability, we help high end manufacturing customers resolve precision mould part bottlenecks, improve mould longevity, production yield and overall market competitiveness.   If you require custom high difficulty micro special shaped tungsten carbide punches and precision mould piercing tools, please feel free to contact us for your dedicated precision  machining solution.  
  • Tungsten Carbide WEDM Finishing Allowance Explained
    Tungsten Carbide WEDM Finishing Allowance Explained Jul 27, 2026
    Having worked with tungsten carbide punches for many years, I'm often asked this question: What is the optimal amount of allowance to leave during the final pass of slow wire drawing precision machining?   To be honest, I used to rely solely on intuition—assuming that any tool would work. That changed when a group of customers reported inconsistent durability: some blades could withstand up to 300,000 uses, while others broke after just 100,000. Upon inspection, the issue turned out to lie in the allowance left during the final blade repair.   Since then, we have tested all five thickness levels—0.01 mm, 0.015 mm, 0.02 mm, 0.025 mm, and 0.03 mm—and today we'll present the results in detail.   Why is the residual allowance during the final blade sharpening process so critical? Slow wire-cutting of tungsten carbide operates on the principle of layer-by-layer removal by electrical discharge. During rough cutting, high energy is applied for rapid processing, but this leaves a "white layer" on the surface—representing re-solidified microstructure. This layer is hard yet brittle and contains microcracks; failure to remove it completely may serve as the initiation point for cracks during stamping.   The final grinding operation aims to completely remove this white layer while achieving a smooth surface with minimal stress.   If the remaining space is too large and the final cut is too deep, new white layers will form, and dimensions may easily deviate from specifications.   The remaining margin is too narrow; the white layer beneath the first cut isn't fully removed, which amounts to ineffective whitening. So, this number must be exactly right.   Our Actual Measurement Data   condition of experiment : Material: KG7 tungsten carbide, thickness 8 mm Wire diameter: 0.25 mm brass wire Rough cutting parameters: Current 12 A, Pulse width 8 μs Cutting parameters: Decrease progressively; reduce the voltage to 40% of the coarse-cutting level on the final pass   Final clearance surface roughness (Ra) White layer thickness dimensional stability overall merit 0.01mm 0.6μm Approximately 2–3 μm in size, with occasional residual particles preferably passing, but unstable 0.015mm 0.5μm Approximately 1–2 μm in size, essentially clean good recommend 0.02mm 0.45μm <1 μm, clean good optimal 0.025mm 0.4μm clean There are slight fluctuations. Available, but size control is more challenging 0.03mm 0.35μm clean The fluctuation is pronounced. Not recommended due to significant size risks     Conclusion: 0.02 mm is the optimal solution. Our tests demonstrate that KG7 tungsten carbide with an 8 mm thickness achieves optimal overall performance when the final tool-sharpening allowance is maintained at 0.02 mm.   Why this number? First, a thickness of 0.02 mm is sufficient to completely penetrate the white layer left by the previous cut. After cutting, the sample was subjected to microhardness testing, and no significant softening layer was observed on the surface.   Second, a cutting depth of 0.02 mm is not significant for tungsten carbide and does not create additional heat-affected zones due to excessive single-discharge energy. The surface roughness can be achieved at approximately Ra 0.45 μm, which is sufficient for the punch application.   Third, it exhibits excellent dimensional stability. Even with a slightly larger allowance (0.03 mm), although the surface becomes smoother, excessive cutting depth may cause fluctuations in wire deflection, leading to reduced dimensional consistency. Given the required tolerance of ±0.002 mm, this risk is not worthwhile.   How to adjust for different thicknesses? Of course, 0.02 mm isn't a universal solution. We've also tested tungsten carbides with varying thicknesses: · For thickness ≤5 mm: the allowance can be set at 0.015 mm, as thin plates dissipate heat rapidly and their white layer is inherently thin.   · For thicknesses of 10–15 mm: It is recommended to reduce the allowance to 0.025 mm, as thicker plates develop a deeper white layer during rough cutting and require an additional margin for complete penetration.   · Thickness>15 mm: We generally do not recommend cutting through the entire thickness in a single pass with slow-speed wire cutting, as this may lead to cracking. Instead, we recommend first performing a wire-cutting operation to create a preliminary groove, leaving a 0.5 mm gap for subsequent grinding on the milling machine. The amount of material left after the final sharpening pass when performing slow wire-cutting on tungsten carbide is not a fixed value; it depends on the material grade, thickness, and rough-cutting parameters.   However, if you are new to this process or lack confidence, starting with a diameter of 0.02 mm is highly unlikely to result in errors. Currently, 90% of our tungsten carbide punches meet this specification, and customer feedback indicates stable service life with a significant reduction in chipping rates.   That's how you make molds—there's no magic formula; it simply comes down to paying close attention to every digit after the decimal point.   If you're also making tungsten carbide punches, feel free to reach out for a discussion. There's no need to place an order—just exchanging insights about the manufacturing process would be great.  
  • How to Cut Tungsten Carbide Punches Without Cracking
    How to Cut Tungsten Carbide Punches Without Cracking Jun 26, 2026
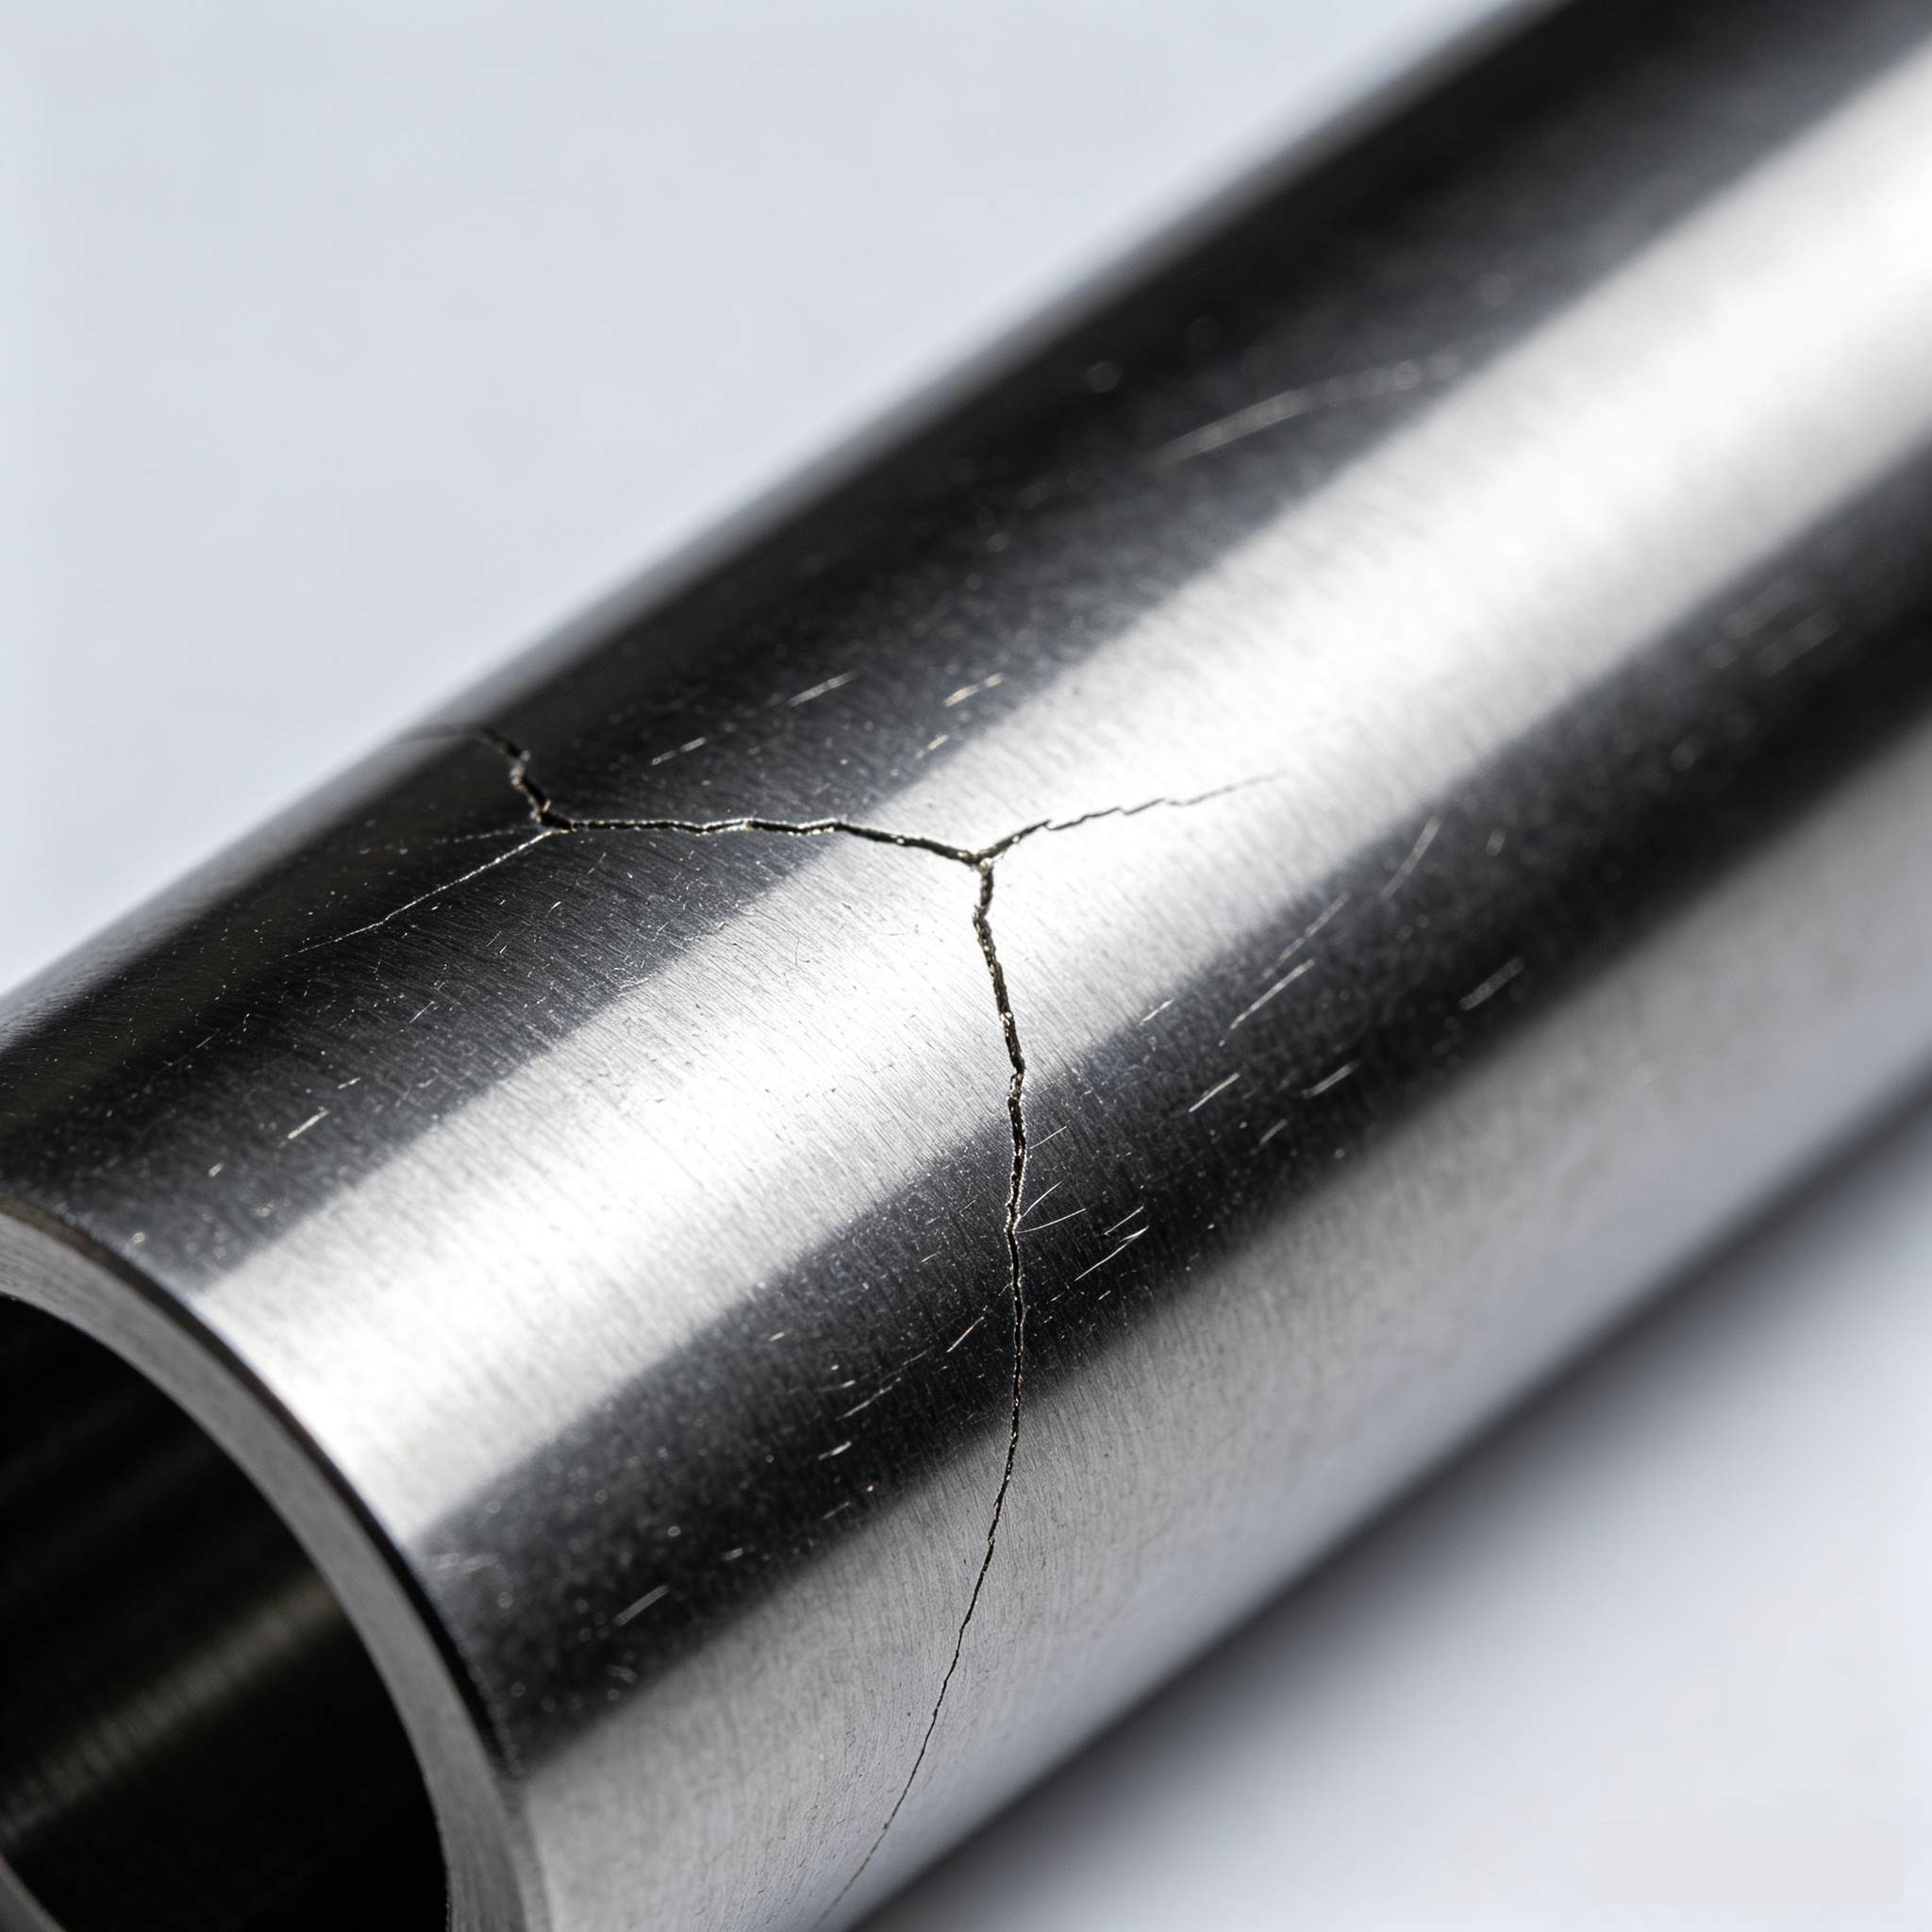
    Why is Tungsten Carbide Prone to Cracking?       Tungsten carbide (hard alloy) is produced by sintering tungsten carbide powder with cobalt binder. Its hardness can reach HRA 89-93, but its elongation is extremely low—in simple terms, it’s “hard but brittle.”     Wire EDM and conventional EDM work by eroding metal with extremely high-temperature electrical sparks. The localized, instantaneous temperatures can reach thousands of degrees, then rapidly cool in the dielectric fluid—this heating and cooling cycle generates thermal stress. If parameters are off, micro-cracks develop on the surface. When the punch is later used in stamping, these cracks propagate under force, causing chipping or complete breakage. Therefore, the key issue with cutting tungsten carbide isn’t whether it can be cut, but how to control heat input and cooling rates.      Wire EDM: Getting the Parameters Right is Paramount     We primarily use wire EDM for manufacturing tungsten carbide punches. The following parameters are non-negotiable:   Don’t Use Excessive Current     Many operators assume higher current means faster cutting. For tungsten carbide, higher current deepens the heat-affected zone and thickens the “white layer” (recast layer). This layer is a breeding ground for cracks.     Our approach: Use moderate current for rough cutting. For finishing, drop the current to a third (or lower) of the roughing value. It is better to make an additional pass than to cut fast and risk thermal cracking.   Keep Pulse Width Short     Longer pulse widths mean higher energy per pulse and faster erosion, but also more damage. We typically control pulse widths between 2–6 microseconds and use sub-2-microseconds for finishing.   Monitor Dielectric Resistivity     If the deionized water’s resistivity is too low, arcing can occur, damaging the work surface. We keep resistivity at 10–15 kΩ·cm; this is checked every shift and the resin is replaced as needed.   Maintain Stable Wire Speed     Too fast and the wire may snap; too slow and chip evacuation suffers. We set speeds between 4–6 m/min, based on wire size and part thickness, ensuring effective flushing without vibration.   Use Multiple Passes as Standard     We always run at least three passes on tungsten carbide punches: rough → finish 1 → finish 2. Cutting energy is reduced with each pass; the final pass is like a gentle “sweep,” producing a near-invisible white layer and an Ra better than 0.8μm.     EDM Drilling: Small Holes are the Most Challenging     Punches may need oil holes or vent holes as small as 0.3 mm—a job for EDM drilling.   The biggest challenge here is chip removal. If debris isn’t flushed, it causes repeated discharge on the hole wall, leading to surface burns or, in severe cases, outright cracking.   Our best practices:   Use straight copper tube electrodes—bent tubes will wander and burn the hole wall. Ensure sufficient flushing pressure so debris is pushed out effectively. Don’t feed too quickly; at the first sign of short-circuiting, retract immediately—never force the electrode.   Post-EDM: What Comes Next?     Cutting is not the end. Two steps are critical after machining:   Inspect the White Layer     We use a magnifier or metallographic microscope to check the edge; if the white layer is visible, we gently polish it off with fine sandpaper. Leaving the recast layer is a hidden trouble for future chipping.   Stress Relieving (Low-Temperature Tempering)     Tungsten carbide punches may retain residual stresses after cutting. If possible, we perform a low-temperature tempering (180–220°C) to effectively release internal stress and stabilize dimensions.     Summary     To “cut” tungsten carbide punches without cracking, it really comes down to three points: Don’t use excessive current; use more finish passes. Ensure effective cooling (flushing) and chip removal. Don’t use the punch straight after machining—inspect the white layer and relieve stress.   This is how we do it at our workshop. Clients call our punches durable and resilient—not because of any “secret trick,” but because we carefully control every process detail.   If you’re struggling with the yield of tungsten carbide punches, let’s discuss—no need for business, sometimes exchanging experience is priceless.
  • Why Do Tungsten Carbide Punches Outperform Steel in High-Speed Stamping?
    Why Do Tungsten Carbide Punches Outperform Steel in High-Speed Stamping? Dec 24, 2025
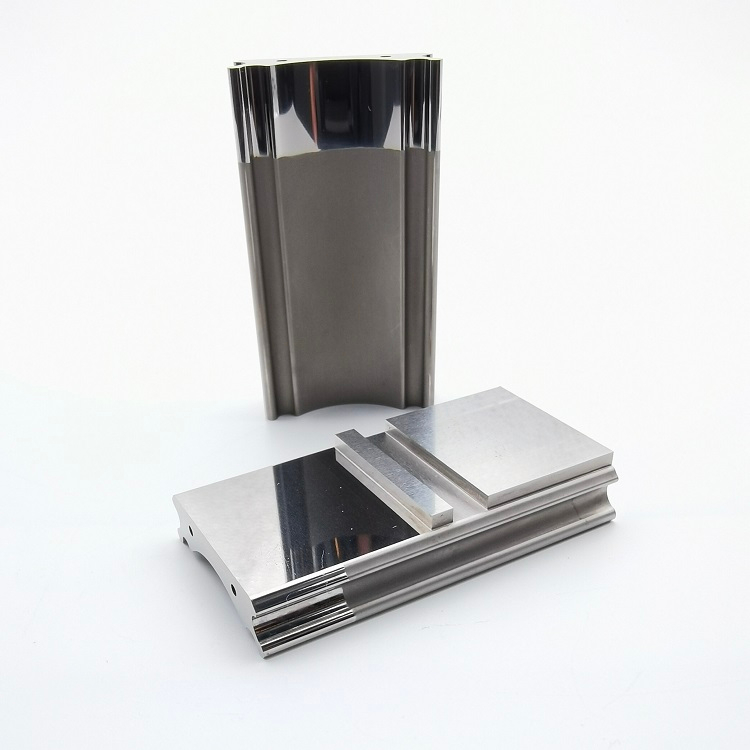
    In the realm of precision manufacturing, high-speed stamping stands out as a core process for mass-producing metal components with high efficiency, tight tolerances and consistent quality, widely used across automotive, electronics, aerospace and hardware industries. To unlock the full potential of this high-frequency, high-intensity machining mode, the performance of stamping die components is crucial — especially punches, the core executing part that directly determines production efficiency, product precision and overall manufacturing costs. Among all punch materials, tungsten carbide has gradually replaced traditional steel as the first choice for high-speed stamping scenarios.   First, let’s clarify the working principle of high-speed stamping dies and the irreplaceable role of punches. High-speed stamping relies on the coordinated operation of upper and lower dies, driven by a high-speed stamping machine to realize continuous stamping, blanking, bending, forming and other processes on metal sheets or strips at a frequency of hundreds to thousands of strokes per minute. The punch, as the core active component of the upper die, directly contacts the workpiece to complete the punching or forming action in each stroke. It bears huge impact force, friction and extrusion force in high-speed, repeated operations, and is required to maintain stable precision without deformation or wear. The quality and material performance of punches not only affect the dimensional accuracy, surface finish of finished parts, but also link to die maintenance frequency, replacement cycle and production line downtime — all of which are critical to enterprise production efficiency and cost control.   When comparing the actual application effects of tungsten carbide punches and traditional steel punches in high-speed stamping, the performance gap is obvious. Traditional steel punches, such as high-speed steel, have certain hardness and toughness, and are low in cost, making them suitable for low-speed, small-batch stamping or processing low-hardness workpieces. However, in high-speed stamping scenarios, their inherent defects are exposed: poor wear resistance leads to rapid edge blunting after short-term high-frequency friction, resulting in reduced precision of finished parts and frequent replacement; low hardness makes them prone to deformation, bending or even fracture under high impact force, affecting production continuity; insufficient corrosion resistance may cause rust or wear acceleration in long-term production, further shortening service life. These problems lead to frequent downtime for die replacement, increased production costs and unstable product quality, which are difficult to meet the high-efficiency, high-precision requirements of modern high-speed stamping production.            In contrast, tungsten carbide punches show unparalleled advantages in high-speed stamping, which is the fundamental reason for their outstanding performance. The first and most prominent advantage is ultra-high hardness and wear resistance. Tungsten carbide has a hardness of HRA 85-93, far higher than traditional steel (HRC 60-65), which can withstand long-term high-frequency friction and impact in high-speed stamping without blunting or wear. This greatly extends the service life of punches, which is 10-50 times that of steel punches, significantly reducing the frequency of punch replacement and production line downtime. Second, it has excellent dimensional stability and high rigidity. Tungsten carbide has a low thermal expansion coefficient, which will not deform due to temperature rise caused by high-speed friction during continuous work, ensuring consistent precision of stamped parts and reducing product defect rates. Third, it has strong impact resistance and extrusion resistance. The dense structure of tungsten carbide enables it to bear huge impact force in high-speed stamping strokes, without bending or fracture, maintaining stable working performance for a long time. Fourth, it has good corrosion resistance, which can resist oxidation and corrosion in harsh production environments, avoiding performance degradation caused by rust and further ensuring service life and product quality. These advantages make tungsten carbide punches perfectly adapt to the high-speed, high-frequency, high-precision working conditions of modern stamping production, effectively improving production efficiency and reducing comprehensive manufacturing costs for enterprises.   As a professional manufacturer of stamping mold components, we have obvious advantages in tungsten carbide punches, focusing on high-quality materials and rich processing experience to provide customers with reliable, high-performance products. In terms of tungsten carbide materials, we mainly adopt imported high-quality raw materials, covering a variety of grades such as fine-grain, coarse-grain and ultra-fine-grain tungsten carbide, which can be customized according to different stamping workpiece materials, thicknesses and stamping speeds to meet diverse production needs. Meanwhile, we have sufficient inventory of various tungsten carbide materials, which can shorten the production cycle and quickly respond to customers’ urgent order demands, avoiding delays caused by material shortages. In terms of processing, we have accumulated years of rich experience in tungsten carbide precision processing, mastering advanced processing technologies such as precision grinding, EDM, and surface coating. Our professional technical team can strictly control the dimensional tolerance and surface finish of punches, ensuring that each tungsten carbide punch meets the high-precision requirements of high-speed stamping. We also can provide customized processing services according to customers’ specific stamping needs, tailoring the most suitable tungsten carbide punch solutions to help customers optimize production efficiency and product quality.                In conclusion, in high-speed stamping scenarios, tungsten carbide punches outperform steel punches in wear resistance, dimensional stability, impact resistance and service life, perfectly meeting the high-efficiency, high-precision production demands of modern manufacturing. Our company relies on imported, diverse and sufficient tungsten carbide materials, as well as rich processing experience, to provide customers with high-quality tungsten carbide punches and customized solutions, helping enterprises reduce production costs, improve product quality and enhance market competitiveness. If you are looking for reliable tungsten carbide punches for high-speed stamping production, we are your trustworthy partner.  
Need Help? Chat with us

leave a message
For any request of information or technical support, fill in the form. All fields marked with an asterisk* are required.
Submit
Looking for FAQs?
Contact us #
+86 769 832011519

Our hours

Mon 11/21 - Wed 11/23: 9 AM - 8 PM
Thu 11/24: closed - Happy Thanksgiving!
Fri 11/25: 8 AM - 10 PM
Sat 11/26 - Sun 11/27: 10 AM - 9 PM
(all hours are Eastern Time)

home

products

whatsApp

Contacts